Directly sourced from premier manufacturing facilities. Engineered for high-frequency commercial catering, luxury hotel chains, and retail brand collections.
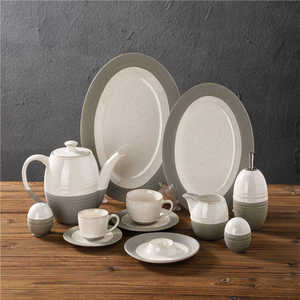
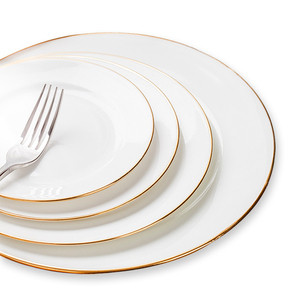
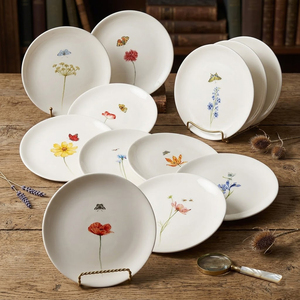
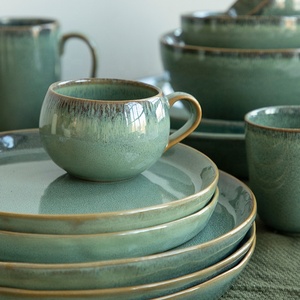
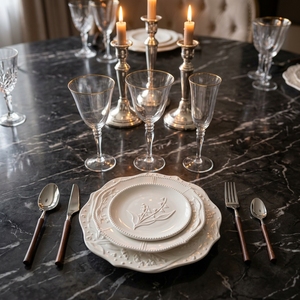
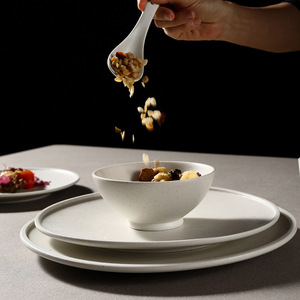
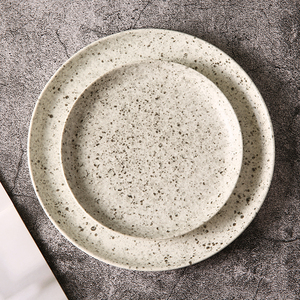
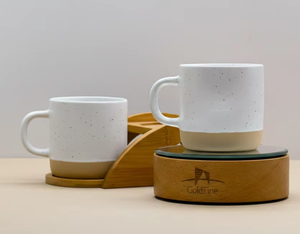
In the evolving landscape of international tabletop procurement, embossed ceramic tableware represents a critical convergence of structural durability, tactile sensory dining experiences, and advanced manufacturing efficiency. Global buyers across hospitality (HoReCa), department store retail, and commercial food services are increasingly shifting away from flat, featureless porcelain toward three-dimensional relief patterning, micro-texture glazes, and sculptured rim profiles.
As premier Chinese tableware factories transition toward Automated Isostatic Pressing and CNC 3D die carving, the precision of embossed ceramic production has reached unprecedented levels. Modern high-temperature vitrification techniques ensure that tactile surface motifs do not compromise mechanical strength, thermal shock parameters, or edge-chip resistance. For procurement officers, understanding the technical nuances of body formulation, mold precision, relief glazing, and international food safety compliance is essential to securing high-margin, reliable inventory for long-term retail and commercial programs.
Achieving sharp, crisp relief relief detailing while maintaining structural vitrification requires specialized machinery, proprietary clay slip recipes, and rigorous micro-shrinkage control.
Utilizing high-pressure hydraulic compaction within flexible elastomeric dies, isostatic forming eliminates internal moisture gradients. This allows complex embossed reliefs—such as radial fluting, geometric diamond knurling, and organic lattice work—to be pressed with uniform green-state density, suppressing warping during high-temperature tunnel kiln firing.
Factory tooling has evolved from manual plaster casting to digital 3D CAD/CAM mold engineering. Direct CNC laser engraving of master aluminum and resin dies enables sub-millimeter precision for intricate botanical embroideries, baroque scrollwork, and contemporary architectural motifs, ensuring batch-to-batch repeatability across multi-container shipments.
Applying glazes over three-dimensional raised ceramic body patterns requires strict surface tension management. Specialized glaze rheology prevents pooling in deep recesses and thin-out along sharp relief ridges. Fired at 1,220°C to 1,260°C, underglazes and reactive glazes interact with tactile crests to create subtle, multi-tonal highlight effects.
Understanding body porosity, firing temperatures, and mechanical strength coefficients allows international buyers to specify the ideal material class for their target commercial or retail applications.
| Material Classification | Water Absorption | Firing Temperature | Modulus of Rupture (MOR) | Thermal Shock Differential | Primary Target Channel |
|---|---|---|---|---|---|
| Vitreous China (High-Alumina) | < 0.5% | 1,240°C – 1,260°C | > 110 MPa | ΔT = 180°C to 200°C | Luxury Hotels, Fine Dining, Commercial Catering |
| Reinforced Fine Bone China | < 0.2% | 1,200°C – 1,230°C | > 130 MPa | ΔT = 160°C to 180°C | Banqueting, Wedding Venues, High-End Retail |
| Earthy Stoneware (Reactive Embossed) | 1.0% – 3.0% | 1,180°C – 1,220°C | > 75 MPa | ΔT = 140°C to 160°C | Nordic Lifestyle Retail, Casual Dining, Mugs |
| Terracotta Serveware | 5.0% – 8.0% | 1,050°C – 1,120°C | > 45 MPa | ΔT = 120°C to 140°C | Rustic Specialty Bakeware, Tapas Serveware |
Modern culinary trends emphasize touch alongside sight and taste. Executive chefs actively specify rimless coupe plates featuring micro-embossed matte bases and tactile satin-glaze borders to elevate food presentation and evoke organic craftsmanship.
Commercial dishwashers and stainless steel cutlery take a heavy toll on traditional flat glazed surfaces. Advanced relief glazes incorporate specialized zirconium silicates to create micro-structure barriers that resist metal marking and scuffing over extended wash cycles.
ESG compliance is shifting buying choices toward suppliers utilizing oxygen-enriched energy-efficient roller kilns and closed-loop clay slurry reclaiming systems. Incorporating up to 25% post-industrial recycled ceramic body solids into embossed stoneware reduces overall carbon footprints without sacrificing structural density.
Exporting high-volume tableware demands stringent in-house laboratory testing to safeguard brand integrity across international markets.
Every raw material batch, slip mix, and glaze slurry undergoes Atomic Absorption Spectrometry (AAS) testing. This guarantees zero extractable lead or cadmium release, fully complying with FDA Compliance Policy Guides, EU Directive 84/500/EEC, California Proposition 65, and GB 4806.4 food contact material directives.
Embossed ceramic pieces are subjected to radical thermal cycling tests—heated to 180°C to 220°C in electric ovens and immediately submerged in 20°C chilled water. Zero crazing, pinhole fracture, or glaze shivering must occur across 5 consecutive shock cycles (BS EN 1183 standard).
From initial hand-sketched artwork or 3D renderings to rapid plaster prototype sampling within 7 to 10 days, our facilities deliver seamless product turnarounds. Full custom backstamp logo branding, retail gift packaging, and barcode integration are standard operating procedures.
Operations are accredited under ISO 9001 (Quality Management Systems) and ISO 14001 (Environmental Management). Facilities undergo annual SMETA (Sedex Members Ethical Trade Audit) compliance inspections, assuring ethical labor practices, workplace safety, and environmental stewardship.
With Authorized Economic Operator (AEO) customs status, container loading and customs documentation are fast-tracked. Our logistics specialists manage FOB, CIF, DDP, and mixed-container consolidated shipments to major ports across North America, Europe, Australia, and the Middle East.