Engineered for high-volume hospitality, retail private-labeling, and specialty food-storage brands. Fully customizable in clay composition, glazes, hermetic silicone sealing, and branded decals.
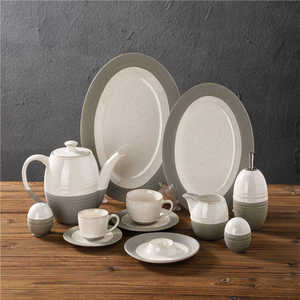
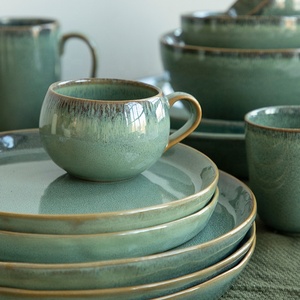
From raw kaolin clay refining to automated roller kiln firing at 1,260°C, our manufacturing facilities integrate precision engineering with stringent quality management.
We utilize ultra-high-pressure powder compacting and CNC-machined master molds to achieve exact dimensional tolerances (+/- 0.5mm), essential for airtight lid engagement on ceramic storage canisters.
Every glaze formulation undergoes rigorous testing via Atomic Absorption Spectrometry (AAS) to verify zero lead and cadmium leaching, ensuring strict compliance with FDA, California Prop 65, and EU 84/500/EEC regulations.
Certified under ISO 9001 and ISO 14001, combined with SMETA ethical trade audits and AEO status. This guarantees expedited international customs clearance and fully audited ethical supply chains.
In modern kitchenware procurement, ceramic storage canisters have evolved from simple utilitarian crocks into complex design elements requiring tight technical integration between ceramic bodies, high-grade glazes, and hermetic sealing mechanisms. For sourcing directors, product engineers, and brand managers, navigating the technical landscape of OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) ceramic canister supply chains requires deep comprehension of material science, kiln thermal dynamics, sealing engineering, and international safety compliance.
Core Procurement Takeaway: Dimensional stability and thermal shock tolerance are the two primary parameters dictating the commercial failure rate of ceramic containers. Ceramic body selection directly governs water absorption metrics, mechanical strength, and lid alignment accuracy.
The operational performance of a commercial canister begins at the raw material slip stage. Depending on target price points, usage environments (pantry storage vs. countertop presentation vs. microwave/oven reheating), and aesthetic requirements, three primary ceramic clay bodies are utilized:
| Material Category | Firing Temp Range | Water Absorption | Modulus of Rupture (MOR) | Primary Commercial Use |
|---|---|---|---|---|
| Vitreous China | 1,220°C – 1,260°C | < 0.5% | High (> 65 MPa) | Luxury Airtight Canisters, HoReCa Professional Storage |
| High-Density Stoneware | 1,180°C – 1,230°C | 1.0% – 3.0% | Medium-High (45–55 MPa) | Retail Lifestyle Kitchen Canister Sets, Decorative Jars |
| Earthenware / Terracotta | 1,000°C – 1,080°C | 5.0% – 10.0% | Moderate (20–30 MPa) | Rustic Bread Bins, Garlic Keepers, Traditional Dry Goods |
For moisture-sensitive goods such as ground coffee, tea leaves, white sugar, and organic spices, Vitreous China and High-Density Stoneware are mandatory to prevent humidity migration through the ceramic body wall. A vitrified clay body fired above 1,220°C converts kaolin, feldspar, and quartz into a dense mullite crystalline matrix interlocked with a glass phase, effectively eliminating open capillary pores.
A major failure mode in retail ceramic canister lines is seal loss caused by out-of-round canister necks mating with rigid lids. Achieving true airtight performance requires precise tolerance engineering across three components:
The visual appeal of ceramic canisters often relies on vibrant glazes—including reactive glazes, matte textures, crackle effects, and metallic lusters. However, glazes containing copper, cobalt, iron oxides, or decorative overglaze decals can release heavy metals if improperly formulated or under-fired.
Our OEM/ODM manufacturing process implements Fritted Glaze Technology, wherein raw glaze components are melted into a glass phase and ground into powder prior to application. This technique locks heavy metallic elements into insoluble silicate structures. Furthermore, our underglaze printing method places decorative pigments beneath a crystal-clear protective silica glaze fired at 1,250°C, rendering the decorated surface 100% scratch-proof and impervious to acidic food attack.
As global retail buyers and hospitality groups recalibrate their supply chain strategies, several critical macro-trends are redefining OEM/ODM ceramic production standards for 2025 and beyond:
Brands are increasingly demanding eco-friendly ceramic collections. Our production facility recycles 100% of unfired greenware clay scrap and filtering sludge back into the raw slip formulation. Furthermore, waste heat from our continuous roller kilns is diverted into raw clay drying rooms, cutting overall factory carbon intensity by 28%.
Consumer preferences have shifted toward versatile products. Modern ceramic canister designs feature oven-to-table thermal shock resistance (withstanding ΔT of 140°C), allowing containers to serve as baking dishes, airtight refrigerator storage containers, and aesthetic serving pieces without thermal cracking.
Integrating AI optical vision inspection on high-speed glazing lines enables real-time detection of pinholes, glaze crawling, and thickness variation prior to kiln entry. This technology drastically lowers factory scrap rates and delivers batch-to-batch color consistency across multi-year reorders.
Bringing a private label ceramic canister collection from initial concept sketch to retail shelf requires a structured, multi-stage development protocol:
Detailed technical and commercial answers addressing common inquiry topics from global buyers, brand managers, and supply chain directors.
Vitreous China is fired at higher temperatures (1,220°C–1,260°C) resulting in a non-porous body with water absorption below 0.5%. It features higher mechanical strength, superior chip resistance, and refined translucency, making it ideal for high-use commercial and luxury applications. Stoneware is fired between 1,180°C–1,230°C with water absorption under 3%, offering a warmer tactile feel, earthier aesthetic, and excellent compatibility with reactive glazes at a lower cost structure.
Standard minimum order quantities for fully customized OEM canister shapes and glazes typically start at 2,000 pieces per shape/color for stoneware, and 3,000 pieces for vitreous china lines. For repeat private-label clients, we offer container consolidation programs where multiple item shapes can be mixed within a single 40ft HQ container to optimize freight costs.
We combine strict CNC mold manufacturing for neck diameter accuracy with custom-molded food-grade silicone gaskets. Every batch undergoes vacuum leak testing and dimensional check gauges to guarantee that neck ovality remains within ±0.75mm, ensuring an airtight seal that protects dry food contents from humidity and ambient air exposure.
Yes. All raw glaze materials are lead- and cadmium-free. We conduct batch-level heavy metal leaching testing using Atomic Absorption Spectrometry (AAS) to verify full compliance with US FDA 21 CFR 175.300, California Proposition 65, and European Union Directive 84/500/EEC standards.
Sample development—including 3D drawing approval, master mold creation, glaze development, and physical pre-production sample release—typically takes 14 to 28 days. Upon sample sign-off and deposit receipt, mass production lead times range from 45 to 60 days depending on order complexity and container volume.
Yes. Our color technicians utilize spectrophotometer color matching to replicate exact Pantone (PMS) reference colors in both matte, gloss, satin, and textured finishes. We also specialize in custom decal transfers, debossed/embossed logos, laser engraving on wooden lids, and custom retail gift box packaging.
Manufacturing in Thailand grants buyers favorable Generalized System of Preferences (GSP) trade status and eliminates punitive section 301 tariffs applicable to other regions. Our factory maintains full AEO (Authorized Economic Operator) certification, accelerating export documentation and customs clearance for Western markets.
Connect directly with our engineering and export team. Receive custom 3D model proposals, glaze sample kits, and factory-direct pricing tailored to your procurement schedule.
Contact Us