Engineered for commercial foodservice networks, luxury hospitality, and high-volume retail buyers globally.
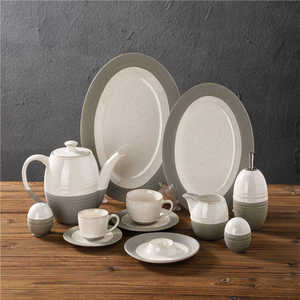
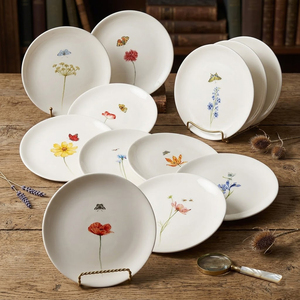
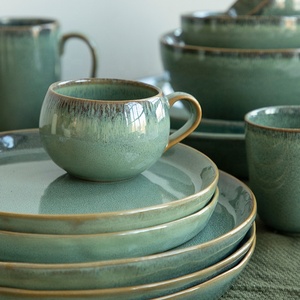
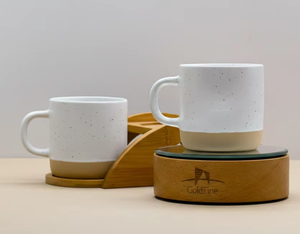
For over three decades, our Southeast Asian production hubs in Bangkok and Ratchaburi have served as strategic partners for premier global dining brands, luxury hotel groups, and international retail chains.
We operate specialized production lines for three core clay bodies: Vitreous China (ultra-dense, high-impact), Stoneware (tactile, thermal resilient), and Terracotta (artisanal, thermal retentive). Each formulation is mixed and refined in-house to guarantee precise mineral stoichiometry.
Certified under ISO 9001 and ISO 14001 systems. Our facilities undergo regular SMETA 4-Pillar ethical audits and maintain Authorized Economic Operator (AEO) status, accelerating international customs clearing for seamless, friction-free B2B deliveries.
We eliminate batch-to-batch variation via state-of-the-art laboratory testing. Every production run is subjected to Atomic Absorption Spectroscopy for heavy metal compliance, spectrophotometric colorimeters, thermal expansion analyzers, and particle-size distribution meters.
| Ceramic Body Type | Firing Temperature Range | Water Absorption Rate | Thermal Shock Resistance | Primary Commercial Target |
|---|---|---|---|---|
| Vitreous China | 1,220°C – 1,260°C | < 0.5% (Non-porous) | Up to 200°C ΔT | High-intensity Commercial Hospitality & Airlines |
| Stoneware | 1,180°C – 1,230°C | < 3.0% (Vitreous interior) | Up to 160°C ΔT | Retail Lifestyle, Fast-Casual Dining, Giftware |
| Earthenware / Terracotta | 1,000°C – 1,150°C | 5.0% – 8.0% (Sealed glaze) | Up to 140°C ΔT | Oven-to-Table Bakeware, Serveware & Rustic Concepts |
| Fine Bone China / Porcelain | 1,280°C – 1,320°C | < 0.1% (High Vitrification) | Up to 220°C ΔT | Luxury Fine Dining, Banqueting & Premium Gifting |
How modern ceramic engineering, automation, and material science are revolutionizing commercial dinnerware production durability and sustainability.
Traditional jiggering and plastic forming often leave internal stress vectors within ceramic body structures, leading to premature warping or edge cracking under high-pressure dishwashing cycles. Modern B2B ceramic manufacturing heavily utilizes Isostatic Dry Powder Pressing.
By subjecting spray-dried ceramic granules to uniform hydraulic pressure (exceeding 300 bar) from all directions simultaneously, the resulting plate greenware exhibits unprecedented density uniformity. This technological shift achieves zero structural anisotropy, reducing dimensional warpage during high-temperature roller kiln firing to less than 0.2% variance.
The global B2B procurement market has shifted decisively toward organic textures and reactive glaze finishes. However, maintaining batch consistency in hand-applied reactive glazes presents immense procurement risk for large-scale hotel chains.
Our automated robotic spray systems combined with computer-controlled multi-zone roller kilns modulate oxygen reduction atmospheres at precise thermal points. This allows complex glaze reactions—such as crystallization, metallic speckling, and matte-satin gradients—to occur with 99.4% repeatable colorimetric profiles across multi-container purchase orders.
Direct high-resolution digital ceramic printing combined with automated water-slide decal applications allows intricate botanical, geometric, and custom logo executions capable of withstanding over 1,500 commercial dishwashing cycles without surface degradation.
Modern continuous roller kilns utilize heat-recovery loops that redirect excess thermal energy from cooling zones back into drying chambers. This reduces total natural gas consumption per kilogram of fired ceramic by up to 32% compared to legacy shuttle kilns.
Industrial closed-loop filter press systems capture 100% of raw glaze runoff and unfired clay trimmings. Reclaimed body materials are re-blended into structural tile or low-porosity core ceramic layers, maintaining zero-landfill ceramic waste standards.
Key shifts shaping how global procurement directors, hotel purchasing executives, and brand owners source ceramic dinnerware.
European and North American retail networks now require comprehensive environmental product declarations (EPDs). Sourcing managers must verify carbon footprints across raw kaolin extraction, kiln firing fuel sources, and transport packaging.
Factories utilizing reclaimed clay bodies and ISO 14001 certified environmental management systems gain preferential vendor ranking. B2B buyers are actively transitioning away from single-fire soft earthenware toward low-emission, ultra-durable vitreous body structures that drastically extend product lifecycles in commercial environments.
The traditional 20-piece formal dinner set has evolved toward modular, multi-functional "blended" dining collections. Coupe plates with deep rims, shallow pasta bowls ("blates"), and stackable ergonomic foot designs dominate current procurement briefs.
Hospitality operators demand stackability features that maximize back-of-house storage efficiency while reducing handling breakage by kitchen staff. High-end buyers are leveraging OEM custom molding to craft bespoke profile lines unique to their brand aesthetic.
With shifting geopolitical trade barriers and fluctuating anti-dumping tariffs on ceramic tableware originating from certain East Asian territories, global buyers are increasingly diversifying supply chains toward established, high-capacity manufacturing centers in Southeast Asia (such as Thailand), securing duty-optimized, risk-mitigated trade corridors.
Food presentation aesthetics favor low-sheen, ultra-durable matte and semi-matte glazes that frame culinary creations without reflecting harsh ambient dining lights. Advanced glazes now integrate microscopic structural additives to prevent cutlery metal-marking on matte surfaces.
Modern procurement extends beyond bulk master cartons. Enterprise buyers expect fully integrated retail-ready solutions: custom barcode printing, eco-friendly molded pulp inserts, ISTA 1A drop-test certified mail-order packaging, and custom backstamps applied prior to container loading.
A whitepaper-grade checklist for procurement teams conducting supplier factory audits and specification sign-offs.
Food contact safety is non-negotiable. Glazes and overglaze decorations must strictly comply with international standards regarding Lead (Pb) and Cadmium (Cd) leaching. Leading factories verify compliance via FDA CPG 7117.06/07, EU Directive 84/500/EEC, and California Proposition 65 limits.
Buyers should demand third-party testing reports (SGS, TUV, Intertek) generated specifically from pre-production batch samples rather than generic material data sheets.
In commercial foodservice, edge chipping is the primary driver of inventory replacement costs. High-performance plates incorporate reinforced rolled edges (rim strengthening) and high-alumina clay formulations.
Standardized testing involves pendulum impact tests (measuring energy resistance in Joules) and Modulus of Rupture (MOR) flexural strength evaluations to ensure the plate body withstands heavy back-of-house busing and high-impact stacking.
Direct answers to the most critical operational, technical, and logistical questions asked by B2B buyers.
For commercial hospitality (HoReCa), Vitreous China is the gold standard. Fired at temperatures between 1,220°C and 1,260°C, its water absorption rate is below 0.5%, making it completely non-porous and highly resistant to bacterial growth, thermal shock, and mechanical edge chipping. Stoneware is an excellent alternative for retail collections or fast-casual concepts desiring a warmer, organic aesthetic, provided it features a fully vitreous glaze application.
Standard OEM production runs typically start at 2,000 to 3,000 pieces per shape and colorway for Stoneware and Terracotta lines, and 3,000 to 5,000 pieces for custom Vitreous China molds. For ongoing contract buyers, mixed-container loading (FCL) can be arranged across multiple SKUs to optimize inventory turns and container load factors.
The standard development cycle spans approximately 90 to 120 days:
1. 3D Modeling & Physical Prototyping: 7–14 days.
2. Master Mold & Glaze Matching: 14–21 days.
3. Pre-Production Sample Sign-Off & Lab Testing: 14 days.
4. Mass Production Firing & Inline Quality Control: 45–60 days.
5. Container Packing & Export Clearance: 7–10 days.
Every batch of raw clay slip and glaze formulation is laboratory-tested via Atomic Absorption Spectroscopy. We certify compliance with US FDA food contact guidelines (CPG 7117.06/07), EU Directive 84/500/EEC, and California Proposition 65. Official test certificates from accredited independent laboratories (SGS / TUV) are provided with shipping documentation for every container.
Yes. Our development studio reverse-engineers glaze chemistry and firing profiles from physical reference samples or Pantone TCX/TPG color codes. Utilizing spectrophotometric colorimeters, we match target hues within tight Delta-E tolerance limits (ΔE < 1.0), ensuring consistent color fidelity across volume re-orders.
We implement a multi-stage Quality Assurance protocol aligned with ISO 9001:
1. Raw Material Verification: Slurry density, viscosity, and particle distribution testing.
2. Greenware Inspection: Automated laser dimensional scan to detect structural warpage before firing.
3. Post-Kiln Inspection: 100% manual ring-test for internal structural cracks, pinhole glaze checks, and color sorting.
4. Packaging Inspection: ISTA 1A drop-testing on sealed master cartons to guarantee zero transit damage during sea freight.
Whether you require full-scale OEM mold development, custom private-label tableware lines, or duty-optimized B2B supply chain solutions, our engineering team is ready to review your project specifications.